In the modern healthcare landscape, patient care optimization has expanded beyond direct medical treatment to encompass the vital segment of home health compliance. Medication Organizers and smart management configurations act as the first line of defense against dosing errors and clinical deterioration. As global populations age, the demand for precision pill organizers, automated medication reminders, and safety-compliant dispensers is growing rapidly.
According to clinical health studies, approximately 50% of medications for chronic diseases are not taken as prescribed. This non-adherence leads to significant clinical complications, increased hospitalization rates, and massive financial burdens on global healthcare systems. To mitigate this risk, B2B procurement professionals, medical institutions, and distributors are increasingly sourcing advanced medication management structures from China’s leading manufacturers, who combine cutting-edge materials science with mechanical and electronic engineering.
Of chronic disease medications are incorrectly administered at home, highlighting the need for structured organizers.
Annual financial impact caused by preventable medical complications stemming from treatment non-compliance.
Achieved when patients use intuitive, multi-compartment, or electronic smart organizers daily.
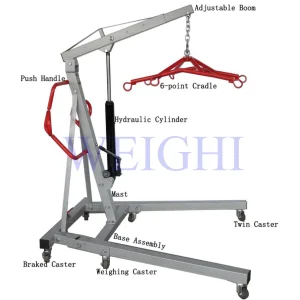
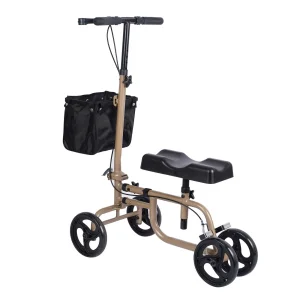
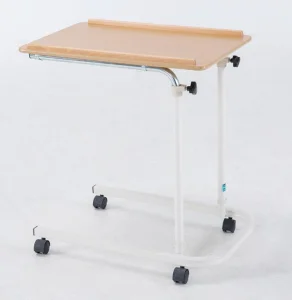
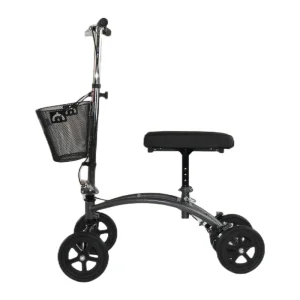
True healthcare accessibility requires a holistic approach to patient autonomy. An optimal aging-in-place layout must integrate tactile medication organizers alongside mobility devices like rollators, patient lifts, and safety grab bars. At Foshan Iowa Medical Technology, we view the patient environment as an integrated system:
By designing products that complement one another, we address both physical mobility and daily pharmaceutical management, ensuring comprehensive safety and peace of mind for families and caregivers.
Foshan Iowa Medical Technology Co., Ltd. is a leading company specializing in the design, production, and innovation of assistive devices for the elderly. Our state-of-the-art factory spans 4,000 square meters, and we are dedicated to providing advanced and comfortable solutions that improve the quality of life for seniors worldwide.
Since our founding, Foshan Iowa has been at the forefront of the assistive medical device industry. We primarily manufacture a range of high-quality products, including crutches, walkers, shower chairs, bedside commodes, toilet armrests, bedside armrests, toilet risers, and other vital mobility aids for the elderly. Our commitment to safety, comfort, and functionality has earned us the trust of customers globally.

We understand that selecting medical products is not only about price. It’s about regulatory compliance, safety standards, and after-sales support. As the demand for elderly care products grows due to an aging population and rising chronic conditions, Foshan Iowa stands out by offering products that meet global safety and quality standards.
Our team is composed of experts in the field of assistive medical devices, from wheelchairs to mobility aids. We employ cutting-edge ergonomic designs and stay ahead of material and manufacturing innovations. Additionally, we ensure that all products meet the highest regulatory standards, ensuring safety, reliability, and peace of mind for both healthcare providers and users.
At Foshan Iowa, we don’t just focus on functionality—we emphasize innovation, safety, and efficiency. Every product undergoes rigorous quality control to meet international standards, providing assurance to both the elderly and healthcare professionals. We aim to improve the daily lives of elderly individuals by providing products that enhance mobility, comfort, and independence.
Core Mission: To leverage technology and craftsmanship to enhance the lives and health of the elderly, ensuring their well-being, safety, and dignity.
Vision: To become a global leader in the innovation of elderly assistive devices, enabling seniors to live freely, with dignity, and without limitations.
Core Values:
Team Culture: At Foshan Iowa, we believe every product reflects our respect for life and the elderly. Every improvement comes from listening to the real needs of those we serve, and every effort contributes to a future where elderly individuals live with dignity, comfort, and independence.
Navigating the complex regulatory landscape of import markets is critical for global distributors. Sourcing medical organizers and assistive systems requires adherence to localized directives. Foshan Iowa products conform to stringent global testing protocols:
Compliance with FDA Class I regulations for medical-grade plastic and mobility aids, ensuring safe utilization in US hospitals and home-care networks.
All items comply with EU Medical Device Regulations, facilitating smooth customs clearance and market insertion throughout EU member states.
Free from BPA, heavy metals, and harmful chemicals, meeting FDA and REACH standards to safeguard patient contact safety.
We also support customized localized language markings, Braille packaging additions for visually impaired patients, and OEM labeling styles to ensure our B2B partners meet their local healthcare retail criteria seamlessly.
Medication organizers and physical safety frameworks must be tailored to their specific environment. Our product lines are optimized for three distinct sectors:
As medical systems transition into the IoT (Internet of Things) era, medication organizers are evolving from passive storage boxes into active healthcare devices. Our innovation roadmap integrates:
Developing Bluetooth and WiFi-enabled pill cases that record extraction timestamps and send real-time alerts to family members or nursing panels.
Integrating silver-ion antimicrobial coatings into standard medical plastics to prevent cross-contamination in high-traffic clinical facilities.
Developing lockable medication cabinets with fingerprint or face recognition systems to prevent accidental double-dosing or unauthorized access.
This continuous R&D cycle ensures that Foshan Iowa clients have access to the latest patient safety innovations, giving them a competitive edge in global procurement tenders.
Foshan Iowa Medical Technology Co., Ltd. is deeply committed to social responsibility. We not only create innovative products but also participate actively in community initiatives that focus on improving the lives of the elderly. We promote aging-friendly transformations within communities, support public welfare actions dedicated to elderly health, and engage in corporate practices that uphold our commitment to social well-being.
We believe in honoring the elderly and recognize our responsibility in supporting their health and independence. Through ongoing efforts, we aim to make the world a warmer, more inclusive place for everyone—especially for the elderly, who deserve to live out their later years with respect, care, and freedom.

 Iowa Medical